
1. Introduction
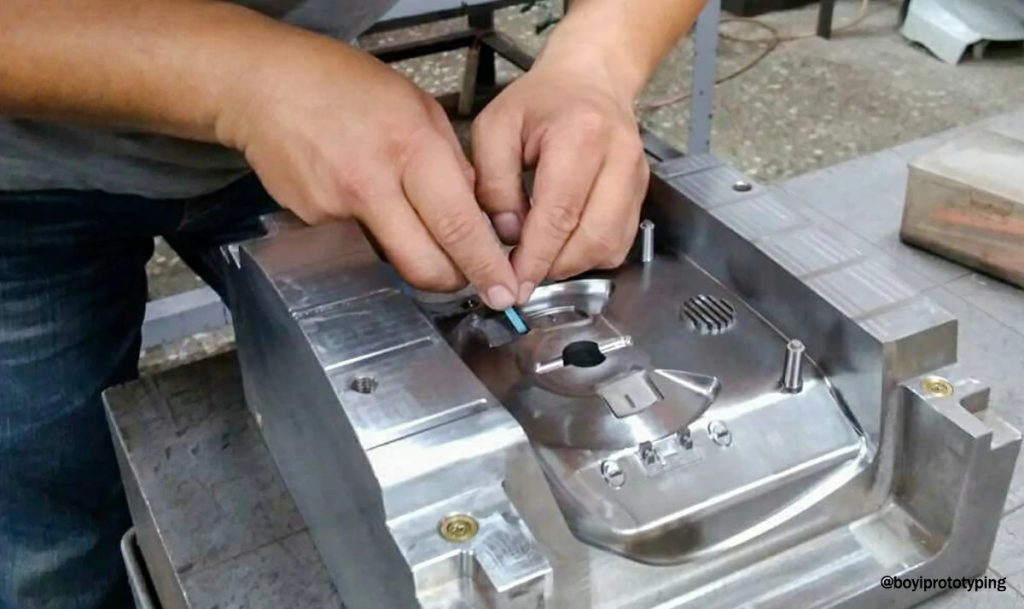
Draft angle is an important design feature in compression moulding because it allows the moulded component to be removed from the mould cavity without excessive force, surface damage, or deformation.
In compression moulding, a measured quantity of moulding material is placed inside a heated mould cavity. The mould closes under pressure, causing the material to flow and fill the cavity. Heat and pressure are maintained for the required curing or processing period. Once the material has sufficiently cured or solidified, the mould opens and the finished component is removed.
Without adequate draft, the component may stick to the mould walls, making demoulding difficult and potentially damaging both the product and the tooling.
A draft angle is the slight taper provided on the vertical or near-vertical surfaces of a mould or moulded component, relative to the direction of mould opening and removal.
Draft angle is particularly important when manufacturing deep components, ribbed parts, containers, housings, and compression-moulded products made from thermosetting materials.
2. Definition of Draft Angle
The draft angle is the angle between a surface and the direction of mould opening, or equivalently, the departure of that surface from a direction parallel to the mould opening axis.
In practical mould design, draft is commonly specified in degrees.
For example, if a cavity wall is designed with a draft angle of 2°, the wall gradually changes its position along the depth of the cavity. This taper reduces contact and friction as the moulded part is withdrawn.
The appropriate draft angle depends on several factors, including:
- Material type and shrinkage behaviour.
- Component depth and geometry.
- Surface finish and texture.
- Mould material and surface condition.
- Demoulding method.
- Dimensional and functional requirements.
Draft is not necessarily required on every surface. Flat surfaces perpendicular to the opening direction may need no draft, while deep walls, ribs, and textured surfaces often benefit from it.
3. Purpose of Draft Angle in Compression Moulds
3.1 Easy Removal of the Moulded Component
The primary purpose of draft is to reduce resistance during demoulding.
A tapered surface provides clearance as the component moves away from the mould, reducing the likelihood of sticking and mechanical interference.
3.2 Prevention of Surface Damage
Insufficient draft can cause scraping, scoring, tearing, or other surface defects during removal.
Providing suitable draft helps preserve the surface finish and dimensional quality of the moulded product.
3.3 Reduction of Ejection Force
When a component has deep, nearly vertical walls, it may grip the mould surface because of shrinkage, friction, or adhesion.
Adequate draft reduces this contact resistance and can lower the force required from ejector pins, mechanical ejectors, or manual removal methods.
3.4 Protection of the Mould Surface
Repeated extraction of tightly fitting parts can cause wear, scratches, or damage to mould surfaces.
A suitable draft angle reduces unnecessary friction and helps extend mould service life.
3.5 Improved Production Efficiency
Easy demoulding reduces interruptions, manual handling, and the time required to remove each component.
This supports more consistent production cycles and reduces the risk of rejected parts.
3.6 Improved Dimensional Consistency
Excessive extraction forces can distort flexible components or damage delicate features. Appropriate draft helps the part release more consistently, supporting dimensional repeatability.
4. Types of Draft Angles in Compression Moulding
Draft may be classified according to the surface being drafted and the direction in which the moulded component is removed.
4.1 External Draft
External draft is applied to the outer walls of a moulded component.
It helps the outside surfaces separate from the corresponding mould surfaces during removal.
Applications:
- External walls of housings.
- Covers and lids.
- Raised projections.
- Outer surfaces of compression-moulded containers.
Advantages:
- Reduces friction during release.
- Helps protect external cosmetic surfaces.
- Supports easier removal from cavity-forming regions.
4.2 Internal Draft
Internal draft is applied to the inner walls of a component, such as recesses, pockets, or enclosed cavity features.
Internal walls may be difficult to release when they grip a core or protruding mould feature.
Applications:
- Internal recesses.
- Hollow sections.
- Pockets and depressions.
- Internal walls formed around mould cores.
Internal draft is particularly important when the material shrinks around a core during cooling or curing.
4.3 Positive Draft
Positive draft generally refers to a taper that widens the opening in the direction of part removal, allowing the component to separate more easily from the mould.
The exact terminology may vary depending on whether the drawing describes the component surface or the mould surface.
4.4 Negative Draft and Undercuts
A negative draft or reverse-tapered feature may create an undercut that prevents straightforward removal along the normal opening direction.
Such features can mechanically lock the component in the mould.
They may require:
- A revised component design.
- A different mould-opening direction.
- Split mould sections.
- Collapsible cores or other specialised tooling.
- A flexible component and a carefully validated release method, where appropriate.
Reverse draft should not be confused with an ordinary, small draft angle. It can fundamentally change how the mould must open.
5. Recommended Draft Angles for Compression Moulds
There is no single draft angle suitable for every compression-moulded component. The required angle depends on material, depth, surface texture, geometry, and release conditions.
The following values are general preliminary design guidelines, not universal manufacturing standards.
| Surface or feature | Illustrative starting range |
|---|---|
| Shallow, smooth walls | 0.5°–1° |
| General external walls | 1°–3° |
| Deep walls | 2°–5° |
| Deep internal recesses | 2°–5° or more |
| Ribbed or detailed surfaces | 1°–3°, subject to geometry |
| Textured surfaces | 3°–5° or more, depending on texture depth |
The final angle should be validated against the selected material and mould design.
For example, a smooth, shallow part made from a material with favourable release characteristics may require relatively little draft. A deep component with textured walls or substantial shrinkage may require a larger angle.
Some simple, shallow features can be produced with little or no draft, but this should be a deliberate design decision supported by the material behaviour, tooling geometry, and demoulding method.
6. Factors Affecting Draft Angle Selection
6.1 Material Type
Different compression moulding materials behave differently during processing and demoulding.
Common materials include:
- Phenolic moulding compounds.
- Melamine-formaldehyde compounds.
- Urea-formaldehyde compounds.
- Epoxy moulding compounds.
- Silicone rubber.
- Natural and synthetic rubber compounds.
Thermosetting compounds generally cure under heat and pressure, while rubber compounds may undergo substantial elastic deformation during removal.
Material shrinkage, stiffness, adhesion, and flexibility all affect the required draft.
6.2 Component Depth
Deeper walls generally require greater attention to draft because the contact area between the moulded part and the tool increases with depth.
A deep cavity with insufficient draft can create high friction and may make the component difficult to remove.
6.3 Surface Texture
Smooth surfaces usually release more easily than heavily textured surfaces.
Texture increases the effective contact area and can mechanically grip the moulded material. Therefore, textured components often require greater draft than smooth components.
6.4 Surface Finish of the Mould
The condition of the mould surface affects release.
Roughness, scratches, deposits, corrosion, and unsuitable surface treatments may increase resistance during demoulding.
A properly finished and maintained mould can improve release, although a smooth surface does not eliminate the need for suitable draft.
6.5 Shrinkage Behaviour
Some materials shrink during cooling or curing. Depending on the geometry, this shrinkage may cause the component to grip a core or other mould surface.
The designer must consider the direction and magnitude of shrinkage, together with the stiffness and flexibility of the moulded part.
6.6 Component Geometry
Ribs, bosses, recesses, thin walls, and narrow channels can complicate demoulding.
Draft must be incorporated without compromising the functional dimensions of the component.
6.7 Demoulding Method
The removal method influences the required draft.
A component removed manually may require a different release arrangement from a component removed using ejector pins or a mechanical extraction system.
However, ejector mechanisms should not be treated as a substitute for appropriate draft where draft is practical.
7. Draft Angle Design in Compression Moulding
Draft should be considered during the early stages of component and mould design.
Step 1: Identify the Direction of Mould Opening
Determine how the mould halves separate and the direction in which the component will be removed.
Surfaces parallel to this direction are the primary candidates for draft.
Step 2: Identify Critical Surfaces
Review the component’s external walls, internal walls, recesses, ribs, bosses, and other features that may contact the mould during removal.
Step 3: Select an Initial Draft Angle
Choose a preliminary angle based on the material, component depth, surface finish, and expected shrinkage.
Use supplier recommendations and established design guidelines where available.
Step 4: Check Functional Dimensions
Adding draft changes the dimensions of tapered surfaces along their depth.
Confirm that critical wall dimensions, mating features, sealing surfaces, and assembly requirements remain within tolerance.
Step 5: Check for Undercuts
Review the component to determine whether any feature prevents straight removal from the mould.
Modify the geometry or provide suitable tooling mechanisms where necessary.
Step 6: Validate the Mould Design
Use CAD analysis to check opening direction, interference, draft continuity, and potential trapped geometry.
Where appropriate, conduct mould trials to evaluate actual release behaviour.
8. Relationship Between Draft Angle and Component Dimensions
Adding draft changes the width or diameter of a component along its depth.
For a simple wall with a constant draft angle, the dimensional change can be calculated using trigonometry.
For one tapered side:
\[ \Delta x = h\tan(\theta) \]
Where:
- \(\Delta x\) = horizontal offset on one side.
- \(h\) = wall depth.
- \(\theta\) = draft angle.
For a symmetrical feature with two opposing walls drafted by the same angle, the total width change is:
\[ \Delta W = 2h\tan(\theta) \]
Example calculation
Suppose a compression-moulded component has a wall depth of 40 mm and a draft angle of 2° on each opposing wall.
\[ \Delta W = 2(40)\tan(2^\circ) \]
\[ \Delta W \approx 2.79\text{ mm} \]
The total width changes by approximately 2.79 mm over the 40 mm depth when both sides taper in the same direction.
This calculation illustrates why draft must be included when defining mould dimensions. The specified width at the top of a feature may differ from its width at the bottom.
9. Common Problems Caused by Incorrect Draft Angles
| Problem | Likely cause | Recommended solution |
|---|---|---|
| Component sticks in the mould | Insufficient draft or high surface friction | Increase draft where feasible and inspect the mould finish |
| Scratches on external walls | Excessive rubbing during removal | Improve draft, check alignment, and remove surface defects |
| Damage to internal recesses | Insufficient internal draft or excessive gripping around a core | Increase internal draft or revise the core design |
| Component distortion | Excessive extraction force or insufficient support | Review draft, ejection arrangement, and component stiffness |
| Difficult manual demoulding | Deep walls, poor release conditions, or inadequate draft | Optimise geometry and evaluate a suitable release system |
| Dimensional variation | Inconsistent demoulding or incorrect compensation for draft | Review tooling dimensions and the release process |
| Mould wear | Repeated forced extraction or abrasive contact | Correct the draft and improve tool maintenance |
| Undercut trapping | Reverse-tapered geometry | Redesign the feature or use an appropriate specialised mould mechanism |
10. Advantages of Proper Draft Angle Design
A properly designed draft angle provides several benefits.
- Easy demoulding: Reduces resistance when removing the finished component.
- Better surface quality: Minimises scratches, scuffing, and tearing.
- Lower ejection forces: Reduces mechanical loading on ejectors and mould components.
- Longer mould life: Limits unnecessary wear and surface damage.
- Improved production efficiency: Reduces cycle interruptions caused by stuck parts.
- Better dimensional consistency: Supports repeatable removal and handling.
- Reduced rejection rates: Helps prevent defects associated with forced extraction.
11. Best Practices for Draft Angle Design
- Include draft in the initial component design rather than adding it at the final tooling stage.
- Select draft according to material properties, wall depth, texture, and release requirements.
- Apply draft to both internal and external walls wherever the geometry requires it.
- Avoid unnecessary reverse-tapered features.
- Consider dimensional changes caused by draft before finalising critical tolerances.
- Maintain appropriate mould surface finish and cleanliness.
- Use CAD draft analysis to identify surfaces that may not release correctly.
- Evaluate deep ribs, narrow recesses, and textured regions carefully.
- Validate draft angles during production trials.
- Investigate material and process conditions as well as geometry when demoulding problems occur.
12. Draft Angle in Compression Moulding Compared with Other Processes
The basic principle of draft is similar across moulding processes, but the design requirements vary.
| Process | Main draft consideration |
|---|---|
| Compression moulding | Release from the cavity or core after curing or solidification |
| Injection moulding | Release after cooling, accounting for shrinkage, ribs, texture, and ejection |
| Thermoforming | Release of the formed sheet from the tool, particularly in deep draws |
| Die casting | Release of the solidified metal casting while accounting for tooling and casting geometry |
| Rubber moulding | Removal of flexible or cured rubber without tearing or excessive deformation |
In compression moulding, draft is especially important for deep thermoset components and parts that shrink tightly around internal mould features.
13. Conclusion
Draft angle is a fundamental design parameter in compression moulds. It provides the taper needed for moulded components to release from the mould with reduced friction, lower extraction forces, and less risk of surface damage.
The correct draft angle depends on the material, component depth, surface texture, mould finish, shrinkage, and demoulding method. Although small angles may be suitable for shallow, smooth components, deep or textured features often require greater draft.
By incorporating draft early in the design process, checking dimensional effects, and validating release behaviour during mould trials, manufacturers can improve product quality, reduce tooling wear, and achieve more reliable compression moulding operations.

