
1. Introduction
The cooling system in injection moulds is one of the most important parts of the injection moulding process. Its main function is to remove heat from the molten plastic after it enters the mould cavity, allowing the plastic to solidify and maintain the required shape and dimensions.
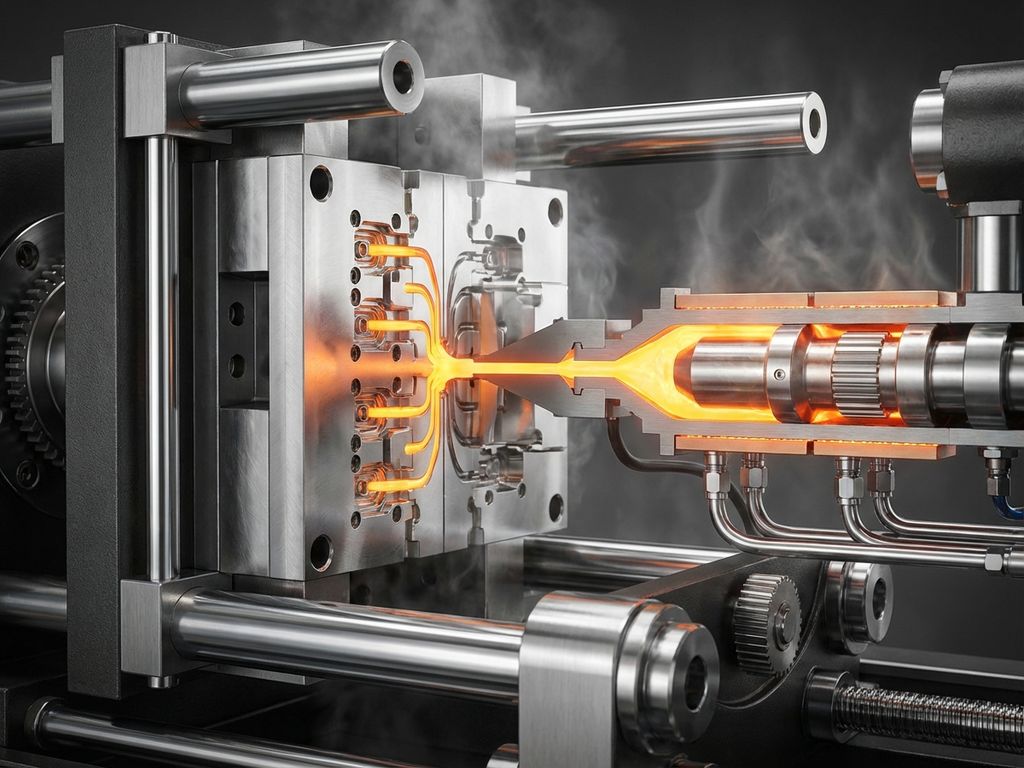
During injection moulding, plastic is heated until it melts and is injected under pressure into a mould. The mould must then cool the plastic sufficiently before the mould opens and the finished component is ejected.
An efficient cooling system helps reduce cycle time, improve product quality, prevent defects, and increase production efficiency.
2. What Is a Cooling System in an Injection Mould?
A cooling system is a network of passages, channels, or cooling elements incorporated into an injection mould. A cooling medium, usually water, circulates through these passages and absorbs heat from the mould.
The absorbed heat is carried away by the circulating fluid and transferred to a cooling unit or temperature-control system.
The cooling system generally consists of:
- Cooling channels
- Inlet and outlet connections
- Water manifolds and fittings
- Hoses or pipes
- Pumps and temperature-control units
- Seals and connectors
The cooling system is designed to maintain a suitable mould temperature throughout the production cycle.
3. Why Is Cooling Important in Injection Moulding?
Cooling is essential for the following reasons.
3.1 Reduces cycle time
Cooling often accounts for a significant portion of the injection moulding cycle. Efficient heat removal allows the plastic component to solidify faster, reducing production time.
3.2 Maintains dimensional accuracy
Uneven cooling can cause different parts of a component to shrink at different rates. This may lead to warpage, distortion, and dimensional variation.
3.3 Improves surface finish
Uniform mould temperature helps produce consistent surface quality and reduces defects such as gloss variation, surface marks, and uneven textures.
3.4 Prevents moulding defects
Proper cooling helps reduce sink marks, warpage, excessive shrinkage, and deformation during ejection.
3.5 Improves productivity
A well-designed cooling system supports consistent production, reduces rejected parts, and can lower energy and operating costs.
4. Main Components of an Injection Mould Cooling System
4.1 Cooling channels
Cooling channels are drilled, machined, or manufactured passages inside the mould plates, cores, and cavities.
Their purpose is to bring the cooling fluid close enough to the hot plastic to remove heat efficiently.
Important design considerations include:
- Channel diameter
- Channel spacing
- Distance from the mould cavity
- Flow rate
- Channel layout
- Ease of cleaning and maintenance
4.2 Cooling medium
The cooling medium transfers heat away from the mould. Common choices include:
- Water: Widely used because of its high heat capacity and good heat-transfer performance.
- Temperature-controlled water: Used when a specific mould temperature must be maintained.
- Water-glycol mixtures: Used in suitable systems where freeze protection or other fluid properties are required.
- Oil: Used in some temperature-control applications where higher operating temperatures are needed.
The medium must be compatible with the mould, pipes, seals, and temperature-control equipment.
4.3 Inlet and outlet connections
The inlet delivers the cooling medium into the mould, while the outlet carries the heated fluid away.
Correct identification and connection are important to prevent leakage, incorrect flow direction, and maintenance problems.
4.4 Manifolds and fittings
Manifolds distribute the cooling medium to multiple channels. Fittings connect the channels to hoses or pipes and help form a reliable, leak-resistant circuit.
4.5 Pump and temperature-control unit
A pump circulates the cooling medium. A temperature-control unit regulates its temperature and may include heating, cooling, filtration, and flow-monitoring functions.
4.6 Seals and plugs
Seals prevent leakage at connections, while plugs close the ends of drilled passages that are not connected directly to external piping.
5. Types of Cooling Systems in Injection Moulds
5.1 Straight-drilled cooling channels
Straight-drilled channels are formed by drilling straight holes through the mould plates.
Characteristics:
- Simple construction
- Relatively low manufacturing cost
- Easy to inspect and clean
- Common in conventional moulds
Limitations:
- May not follow the shape of complex components
- Can leave hot spots in areas far from the channels
- Cooling may be uneven around complicated cores
These channels are commonly used for flat components and relatively simple mould geometries.
5.2 Baffle cooling system
A baffle is a thin metal plate inserted into a cooling passage to divide the flow into two paths. Coolant travels down one side of the passage and returns through the other.
Advantages:
- Improves cooling in deep mould sections
- Can reach areas that are difficult to cool with straight channels alone
- Relatively simple to manufacture
Limitations:
- Flow resistance may be higher
- Baffles must be designed and installed correctly
- Cleaning can be more difficult in some arrangements
5.3 Bubblers cooling system
A bubbler is a tube installed inside a larger cooling passage. Coolant travels down the tube, exits near the bottom, and returns through the surrounding space.
Bubblers are especially useful for cooling deep cores and narrow mould features.
Advantages:
- Effective for slender cores
- Improves heat removal from deep areas
- Can reduce local hot spots
Limitations:
- Requires careful sizing and installation
- Pressure loss can be significant
- Tubes may need inspection or cleaning
5.4 Spiral cooling system
A spiral cooling passage guides coolant along a curved or helical path around a core or other mould feature.
It is used when heat must be removed from a cylindrical or elongated region.
Advantages:
- Can provide more uniform cooling around curved surfaces
- Useful for cylindrical cores and similar features
Limitations:
- More difficult to manufacture than simple drilled channels
- Flow distribution and cleaning require attention
5.5 Conformal cooling system
Conformal cooling channels follow the shape or contour of the mould cavity more closely than conventional straight-drilled channels.
They are often produced using metal additive manufacturing, although specialized manufacturing methods may also be used.
Advantages:
- Can improve temperature uniformity
- Can reduce local hot spots
- May shorten cooling time
- Particularly useful for complex geometries
Limitations:
- Higher manufacturing cost
- More complex design and simulation requirements
- Internal passages can be difficult to inspect and clean
Conformal cooling is especially beneficial when conventional channels cannot provide adequate cooling uniformity.
5.6 Series cooling system
In a series arrangement, coolant passes through one channel or cooling section after another.
Advantages:
- Simple plumbing
- Flow through each section is easy to conceptualize
- Can be suitable for small or uncomplicated moulds
Limitations:
- Coolant becomes progressively warmer as it travels through the circuit
- Pressure drop increases along the flow path
- Downstream regions may receive less effective cooling
5.7 Parallel cooling system
In a parallel arrangement, coolant is distributed through several separate channels connected to common supply and return manifolds.
Advantages:
- Can provide more uniform coolant inlet temperatures across circuits
- Allows separate circuits to cool different mould regions
- Can improve control over complex mould layouts
Limitations:
- Flow may distribute unevenly between channels
- Each circuit may need balancing
- Manifolds and connections can increase system complexity
6. How the Cooling System Works
The cooling process takes place in several stages.
- Plastic injection: Molten plastic enters the mould cavity under pressure.
- Heat transfer: Heat moves from the hot plastic into the mould steel or other mould material.
- Coolant circulation: The cooling medium flows through the internal channels and absorbs heat from the mould.
- Heat removal: The warmed coolant leaves the mould and transfers heat to a cooling unit or heat exchanger.
- Plastic solidification: The plastic becomes sufficiently rigid to retain its shape.
- Mould opening: The mould opens after the required cooling and holding stages.
- Part ejection: The finished component is ejected, and the next cycle begins.
Cooling must be sufficient for the part to withstand ejection forces without deforming.
7. Important Design Factors
7.1 Cooling channel diameter
The diameter affects coolant velocity, pressure drop, and heat-transfer performance.
- Very small channels may create excessive pressure loss and be more vulnerable to blockage.
- Very large channels may require more space and may not provide the desired local heat-transfer performance.
The optimum diameter depends on the mould dimensions, flow requirements, available pressure, and manufacturing constraints.
7.2 Distance from the mould cavity
Cooling channels must be positioned close enough to remove heat effectively without weakening the mould structure.
Channels placed too far away may result in slow cooling. Channels placed too close to the cavity may compromise strength or cause local temperature variations.
7.3 Channel spacing
Spacing determines how evenly heat is removed across the mould.
Excessive spacing can create hot spots, while insufficient spacing can complicate manufacturing and weaken the mould.
7.4 Coolant flow rate
The flow rate influences heat removal and temperature uniformity.
A suitable flow rate depends on channel geometry, coolant properties, temperature rise, and pressure drop. Turbulent flow often improves heat transfer compared with laminar flow, although it also affects pumping requirements.
7.5 Mould material
The thermal conductivity of the mould material affects how quickly heat moves from the cavity surface to the cooling channels.
Tool steels are widely used for durability and strength, while certain copper alloys may be used in selected areas where improved thermal conductivity is beneficial.
7.6 Plastic material
Different plastics have different processing temperatures, thermal properties, shrinkage behaviour, and solidification characteristics.
For example, semicrystalline plastics such as polypropylene and polyethylene may require different cooling considerations from amorphous plastics such as polystyrene or ABS.
7.7 Part geometry and wall thickness
Thick sections generally require more cooling time than thin sections. Ribs, bosses, deep cores, and changes in wall thickness can produce uneven heat distribution.
Cooling should therefore be designed around the actual component geometry rather than simply using uniform channel spacing everywhere.
7.8 Temperature difference
The difference between the mould temperature and the coolant temperature affects heat-transfer rate. However, excessively cold coolant may cause condensation, thermal stress, or undesirable surface-quality effects in some applications.
The aim is controlled and uniform cooling, not necessarily the lowest possible coolant temperature.
8. Cooling System Design Guidelines
When designing a cooling system, engineers should consider the following practices:
- Place channels strategically around thick sections and expected hot spots.
- Use separate circuits for areas with different cooling requirements.
- Maintain consistent channel spacing where practical.
- Avoid sharp bends and unnecessary restrictions that increase pressure loss.
- Ensure that coolant can flow through every intended channel.
- Provide access for cleaning, flushing, and inspection.
- Use corrosion-resistant materials and suitable water treatment where required.
- Consider mould strength, ejector pins, inserts, slides, and other internal components when routing channels.
- Use thermal simulation or mould-flow analysis for complex moulds.
- Verify flow rate, pressure drop, and temperature distribution during commissioning.
9. Common Cooling System Defects and Their Solutions
| Problem | Possible cause | Recommended solution |
|---|---|---|
| Warpage | Uneven cooling or uneven shrinkage | Improve channel layout and balance coolant flow |
| Sink marks | Thick sections or inadequate packing and cooling | Review wall thickness, packing conditions, and cooling time |
| Long cycle time | Insufficient heat removal or low coolant flow | Improve channel design, check flow, and optimize cooling conditions |
| Hot spots | Cooling channels too far from critical areas | Add or reposition channels where structurally feasible |
| Leakage | Damaged seals, loose fittings, or cracked passages | Replace seals, tighten suitable connections, and inspect the mould |
| Scale or blockage | Poor coolant quality or corrosion products | Flush channels and improve water treatment |
| Uneven surface gloss | Temperature variation across the cavity | Balance coolant distribution and stabilize mould temperature |
| Part sticking during ejection | Insufficient solidification or unsuitable ejection conditions | Optimize cooling and review the ejection system |
These defects may also have causes unrelated to cooling. For example, sink marks can result from insufficient packing pressure, while warpage can also be caused by material orientation and part design.
10. Factors Affecting Cooling Time
Cooling time depends on several factors:
- Part wall thickness: Thicker sections generally take longer to cool.
- Plastic thermal properties: Thermal conductivity, heat capacity, and solidification behaviour affect cooling.
- Mould temperature: Higher mould temperatures often increase the time needed to reach the ejection condition.
- Coolant temperature: Lower inlet temperatures may increase the temperature difference and heat-transfer rate, within suitable process limits.
- Channel layout: Channels close to important heat-generating regions can improve cooling effectiveness.
- Coolant flow: Insufficient flow may allow the coolant to warm excessively or reduce heat-transfer performance.
- Required ejection temperature: The component must be sufficiently rigid to avoid deformation during ejection.
Cooling time should be established through process trials, calculations, and simulation where appropriate. Simply increasing cooling time may hide an inefficient cooling layout rather than solve it.
11. Maintenance of the Cooling System
Regular maintenance is essential for stable production and long mould life.
Daily or routine checks
- Check for coolant leakage.
- Confirm that inlet and outlet temperatures are within the required range.
- Verify that flow indicators and pressure readings are normal.
- Check hoses and fittings for damage.
Periodic maintenance
- Flush cooling channels as required.
- Inspect filters and clean or replace them.
- Check water quality and corrosion levels.
- Inspect seals, connectors, and manifolds.
- Measure flow through individual circuits where possible.
- Remove scale and deposits using methods compatible with the mould materials.
Blocked channels can significantly reduce cooling performance even if the temperature-control unit appears to be operating normally.
12. Advantages of an Efficient Cooling System
An efficient cooling system provides several benefits:
- Shorter moulding cycle times
- Higher production output
- Better dimensional stability
- More consistent surface finish
- Reduced warpage and deformation
- Lower rejection rates
- More consistent processing conditions
- Potential reductions in energy consumption and operating cost
13. Limitations and Challenges
Despite its benefits, cooling system design can involve several challenges:
- Limited space inside the mould
- Interference with ejector pins, slides, and inserts
- Difficult-to-cool deep cores
- Uneven coolant distribution
- Corrosion and mineral deposits
- High costs associated with complex or conformal channels
- Difficulty inspecting inaccessible internal passages
- The need to balance cooling performance against mould strength and durability
These challenges are addressed through careful design, simulation, appropriate material selection, and regular maintenance.
14. Applications
Cooling systems are used in injection moulds for manufacturing a wide range of plastic products, including:
- Automotive interior and exterior components
- Electronic housings and enclosures
- Household appliance parts
- Packaging caps and containers
- Medical plastic components
- Toys and consumer products
- Industrial plastic fittings
- Thin-wall packaging components
The cooling layout varies depending on component size, shape, material, production volume, and dimensional requirements.
15. Conclusion
The cooling system is a critical part of an injection mould because it controls heat removal, solidification, dimensional stability, and cycle time.
Straight-drilled channels are suitable for many conventional moulds, while baffles and bubblers help cool difficult-to-reach areas. Spiral and conformal cooling designs can provide better heat removal in selected complex geometries.
The main objective is to achieve fast, uniform, and controlled cooling without compromising mould strength or product quality. Proper design, balanced coolant flow, suitable temperature control, and regular maintenance help ensure efficient and reliable injection moulding production.

