
1. Introduction
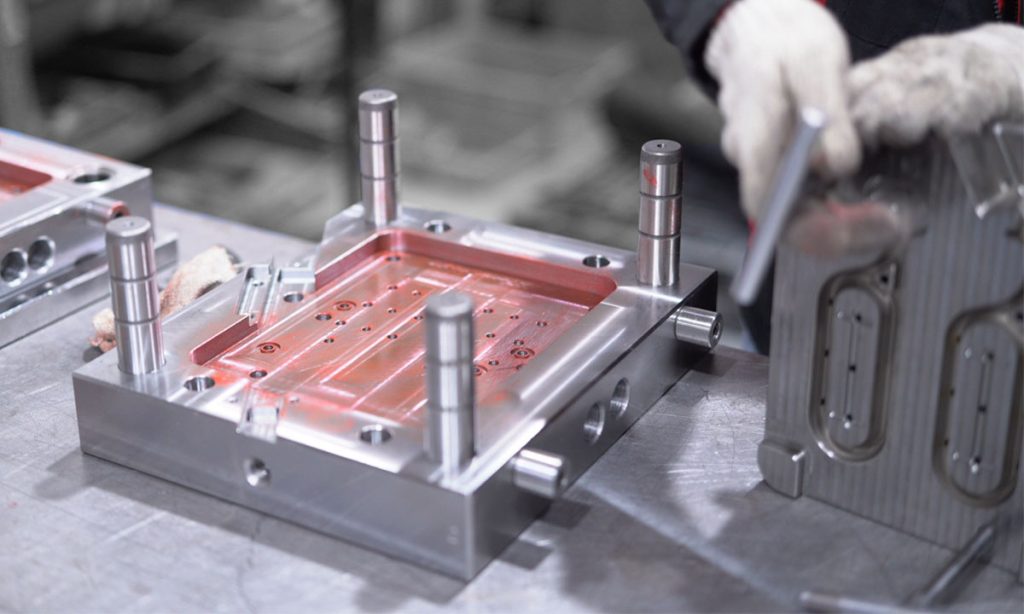
A draft angle in injection mould design is a slight taper provided on the vertical surfaces of a moulded part to help it release easily from the mould after the plastic has cooled and solidified. Instead of designing the walls perfectly parallel to the direction of mould opening, a small angle is introduced to reduce friction between the plastic component and the mould surface.
Draft angle is an important design consideration because plastic materials can shrink around the mould core during cooling. Without sufficient draft, the part may stick to the mould, require excessive ejection force, develop scratches, or become permanently damaged during removal.
Proper draft angle selection improves moulding efficiency, product quality, mould life, and production consistency.
2. Why Is Draft Angle Required?
During injection moulding, molten plastic is injected into a closed mould cavity under pressure. The plastic cools and solidifies, then shrinks as its temperature decreases.
Depending on the geometry, the plastic may grip the core or cavity surface. Draft creates a gradual clearance between the mould surface and the component as the mould opens.
The main purposes of draft angles are:
- Easy demoulding: Allows the plastic part to release smoothly from the mould.
- Reduced friction: Minimises rubbing between the component and the mould walls.
- Prevention of scratches: Helps avoid drag marks and scuffing.
- Lower ejection force: Reduces the force required from ejector pins or other release mechanisms.
- Improved surface finish: Protects textured, polished, or decorative surfaces.
- Reduced mould wear: Minimises friction-related wear on the mould.
- Higher production efficiency: Helps reduce sticking problems and interruptions during production.
3. What Is a Draft Angle?
A draft angle is the angle between a moulded part’s sidewall and the direction in which the part is removed from the mould.
For example, if a plastic component has vertical walls with no taper, its draft angle is approximately \(0^\circ\). If the walls taper slightly outward in the direction of removal, the component can release more easily.
Draft angles are usually measured in degrees.
Typical starting points for many injection-moulded plastic parts are:
| Surface type | Typical starting draft |
|---|---|
| Smooth, polished surface | 0.5°–1° |
| General-purpose surface | 1°–2° |
| Deep walls or increased sticking risk | 2°–3° or more |
| Lightly textured surface | 1°–3° |
| Heavily textured surface | 3°–5° or more |
These values are general guidelines, not universal requirements. The correct angle depends on the plastic material, wall depth, surface finish, texture depth, shrinkage, mould construction, and ejection arrangement. Some applications require larger angles, while precision features may need specialised design and testing.
4. How Draft Angle Works
The draft angle helps create clearance between the moulded part and the mould surface during ejection.
The process can be understood in four stages:
- Mould filling: Molten plastic enters the cavity and fills the required geometry.
- Cooling and shrinkage: The plastic solidifies and contracts as it cools.
- Mould opening: The mould halves separate along the intended opening direction.
- Part ejection: The component moves away from the core or cavity, with the draft reducing interference and friction along the walls.
A larger draft angle generally improves release, but it can also change the component’s dimensions. Designers must balance easy ejection with functional and visual requirements.
5. Types of Draft Angles in Injection Mould Design
5.1 External Draft
External draft is applied to the outside walls of a moulded component.
It allows the outer surface to release from the cavity side of the mould.
Applications:
- Plastic containers
- Covers and housings
- Storage boxes
- Decorative components
- Plastic trays
Benefits:
- Easier release from the cavity
- Reduced surface scratching
- Lower risk of sticking during ejection
5.2 Internal Draft
Internal draft is applied to the inside walls of a component, such as the inner walls of a cup or container.
These surfaces are commonly formed around the mould core. Plastic shrinkage may grip the core, making internal draft especially important.
Applications:
- Cups and tubs
- Plastic caps
- Containers
- Hollow housings
- Enclosures with internal walls
Benefits:
- Easier removal from the core
- Reduced ejection resistance
- Lower risk of deformation and internal scuffing
5.3 Draft on Textured Surfaces
Textured surfaces require careful draft selection because surface features can mechanically resist movement during ejection.
The deeper or more pronounced the texture, the greater the draft generally required to prevent the texture from dragging against the mould.
Applications:
- Textured housings
- Consumer-product enclosures
- Decorative plastic panels
- Non-slip plastic components
Important: The required draft depends on the texture specification and the mould texture supplier’s recommendations. The angle should be established before texturing the mould surface.
5.4 Draft on Polished Surfaces
Polished surfaces can often be designed with relatively small draft angles because their smooth finish reduces mechanical resistance.
However, highly polished surfaces can still experience vacuum effects, adhesion, or sticking caused by shrinkage and part geometry.
Applications:
- Transparent plastic components
- Optical or appearance-critical parts
- Smooth covers and housings
- Gloss-finish consumer products
The draft angle must still be sufficient to release the part without damaging its surface.
5.5 Draft on Deep Ribs and Walls
Deep ribs, narrow slots, and tall walls can create substantial friction during ejection.
These features often require additional draft to allow the part to move away from the mould without binding.
Design considerations:
- Wall depth
- Rib thickness
- Distance from the mould opening direction
- Material shrinkage
- Ejector-pin position
- Required surface quality
6. Factors Affecting Draft Angle Selection
6.1 Plastic Material
Different plastic materials have different shrinkage rates, stiffness, flexibility, and friction characteristics.
For example, a flexible plastic may release differently from a rigid plastic, while some materials shrink tightly around the core.
The draft angle should therefore be selected for the actual material grade rather than relying on a generic value.
6.2 Part Depth
Deeper walls generally require more draft because the plastic contacts a greater length of the mould surface.
A shallow component may release successfully with a small draft, while a deep container may need a larger angle to avoid excessive friction.
6.3 Surface Finish
Surface finish has a direct effect on demoulding.
- Smooth, polished surfaces may allow smaller draft angles.
- Matte finishes may require additional draft.
- Textured surfaces generally need greater draft, depending on texture depth and geometry.
6.4 Shrinkage
As plastic cools, it contracts. In many part geometries, this causes the material to grip the core more tightly.
Materials with greater moulding shrinkage may require additional attention to draft, core geometry, and ejection design.
6.5 Wall Thickness
Wall thickness affects cooling, shrinkage, and dimensional stability. Although draft is primarily a geometric consideration, wall thickness can influence how the component behaves during ejection.
Sudden wall-thickness changes should be avoided where possible because they may cause uneven cooling and distortion.
6.6 Ejection System
The type and location of the ejection system also influence draft requirements.
Ejector pins, stripper plates, sleeves, and air-assisted release systems each interact differently with the component. Insufficient draft may cause local stress, ejector marks, or deformation.
7. How to Calculate Draft Angle
Draft angle can be calculated from the change in wall dimension over a given height.
For a wall that tapers on one side:
\[ \theta = \tan^{-1}\left(\frac{\Delta x}{h}\right) \]
Where:
- \(\theta\) = draft angle
- \(\Delta x\) = horizontal change in the wall position on one side
- \(h\) = wall height
Example:
Suppose a plastic component has a wall height of 50 mm and the wall moves outward by 1 mm over that height.
\[ \theta = \tan^{-1}\left(\frac{1}{50}\right) \]
\[ \theta \approx 1.15^\circ \]
Therefore, the draft angle is approximately \(1.15^\circ\).
For a symmetrical part that tapers on both sides, be careful to distinguish the dimensional change on one side from the total change in width. The calculation above uses the change on one side.
8. Problems Caused by Insufficient Draft Angle
Insufficient draft can lead to several manufacturing defects.
| Problem | Cause | Possible solution |
|---|---|---|
| Part sticking | Insufficient clearance during ejection | Increase draft where design permits |
| Scratches or drag marks | Plastic rubs against the mould surface | Improve draft and mould finish |
| Part deformation | Excessive ejection force | Increase draft and optimise ejection |
| Ejector-pin marks | High force concentrated at ejector locations | Review draft, ejector placement, and cooling |
| Surface damage on texture | Textured features drag during release | Increase draft according to texture requirements |
| Longer cycle time | Repeated sticking or difficult ejection | Optimise draft, cooling, and release conditions |
| Mould wear | Excessive friction during repeated ejection | Improve draft and maintain the mould surface |
Increasing the draft angle is not always the only solution. Cooling conditions, surface finish, mould alignment, venting, shrinkage, and ejector layout should also be reviewed.
9. Best Practices for Draft Angle Design
- Establish the mould opening and part-removal direction early in the design process.
- Apply draft to all surfaces parallel or nearly parallel to the direction of ejection where practical.
- Use larger draft angles for deeper walls and textured surfaces when required.
- Confirm the material grade and its shrinkage behaviour.
- Coordinate draft requirements with the surface-texture specification.
- Avoid abrupt transitions in wall geometry.
- Check draft using CAD draft-analysis tools before manufacturing the mould.
- Ensure that ribs, bosses, slots, and other internal features can release properly.
- Consider the positions of ejector pins and other release mechanisms.
- Validate the design through mould trials and inspect the finished parts for drag marks or deformation.
10. Draft Angle in Candle-Mould Manufacturing
Draft angle is also relevant to moulds used for manufacturing certain candle shapes, especially pillar candles with tapered or detailed sidewalls.
A suitable taper can help the finished candle release from a rigid mould. However, candle wax behaves differently from injection-moulded thermoplastics, so the draft angle must be chosen according to the wax formulation, candle geometry, mould material, cooling shrinkage, and demoulding method.
For injection-moulded plastic tooling used to manufacture candle accessories, such as candle holders or containers, draft should be designed according to the plastic material and the requirements of the injection-moulding process.
11. Conclusion
Draft angle is a fundamental element of injection mould design that helps plastic components release smoothly from the mould after cooling. It reduces friction, lowers ejection forces, protects surface quality, and improves production efficiency.
The correct draft angle depends on the material, part depth, surface texture, shrinkage, wall geometry, and ejection method. Applying appropriate draft during the design stage helps prevent sticking, scratching, deformation, and unnecessary mould wear while supporting consistent, high-quality production.

